
 HOTLINE:+8613974960765 +8618507312158 HOTLINE:+8613974960765 +8618507312158


— Knowledge —
— PRODUCTS —
 Service Hotline +8613974960765
Email:susie@hnljpump.com
Mobile:+8618507312158
TEL:+8613974960765
Right Angle Gearboxes
Publication date:2025/1/29 23:56:37 popularity: [content:visits]
This case study focuses on the joint fire protection system renovation project of a super high-rise commercial complex and a large petrochemical industrial park. The H-series right angle gearbox is used to drive the diesel engine vertical long axis fire pump, which solves the core pain points of traditional motor direct coupled fire pumps such as limited layout in underground spaces and unreliable power-off start-up. It fully meets the national standard requirements of GB6245 fire pumps and achieves 100% emergency response reliability of the fire protection system.
🏢 Project background and original pain points
The project includes a 328 meter super high-rise commercial complex and a supporting chemical park fire pump station. The original fire protection system used a conventional motor directly connected vertical fire pump scheme, which exposed multiple fatal safety hazards during operation:
The underground pump room space is seriously insufficient: the floor height of the underground fire pump room in super high-rise buildings is only 3.6 meters, and the vertical motor is directly stacked above the pump body. The total axial height of the unit exceeds 3.3 meters. During daily maintenance, there is insufficient space for crane lifting, and dismantling the pump body requires temporary removal of the top pipeline of the pump room. A single maintenance takes more than 72 hours, and the fire protection system is in a non standby state for a long time.
Risk of failure during power outage startup: The probability of power outage in super high-rise buildings and chemical industrial parks is high, and the original motor direct connection scheme relies on power supply from the city. The response time for the backup generator to start is as long as 30 seconds, which cannot meet the mandatory standard of 5 seconds for the pump set to start and reach the rated pressure required by fire safety regulations.
Frequent axial thrust overload faults: The fire pump has a rated flow rate of 300L/s and a head of 200m, generating a maximum axial thrust of 85000N during operation. The original vertical fire motor has a thrust bearing with a rated load of only 55000N, and bearing burnout occurs on average after 10 months of long-term overload operation. The unplanned failure rate of the fire pump is as high as 15%.
Poor adaptability to explosion-proof scenarios: In the explosion-proof area of the chemical industrial park, the electrical components of ordinary motor directly connected fire pumps are close to flammable and explosive media, and the sealing failure can easily cause explosion safety accidents, which completely does not comply with the explosion-proof safety regulations of the petrochemical industry.
🛠️ Customized selection scheme for H-series right angle gearbox
For the special working conditions of this fire protection project, a dual scenario customized upgraded H-series right angle gearbox is selected, and the core configuration fully meets the strict requirements of the fire protection system:
Accurate matching of core parameters:
Suitable for diesel engine input power of 800HP (approximately 597kW), with 25% power redundancy reserved, rated input speed of 1500rpm, and customized transmission ratio of 1.5:1 to achieve pump output speed of 2250rpm, fully matching the operating point of fire pump rated flow rate of 300L/s and head of 200m.
Upgraded heavy-duty thrust roller bearings, with a rated axial thrust bearing capacity of 125000N, fully covering the maximum axial thrust of 85000N during the operation of the fire pump, and reserving 47% of the thrust redundancy, completely solving the problem of overload of the original motor bearings.
Optimization of Fire Protection Special Structure:
The gears are made of 20CrMnTi alloy steel and undergo carburizing and quenching treatment. The precision has been upgraded to level 6, and the transmission efficiency reaches 97%. The high torque output characteristic ensures that the fire pump accelerates from static to rated speed within 3 seconds, instantly reaching the rated pressure.
Equipped with a mandatory oil injection lubrication system, even under the instantaneous full load impact condition of the pump unit, all gear meshing surfaces can still form a complete oil film, avoiding instant dry wear and damage to the tooth surface. The protection level has been upgraded to IP55, and the shaft end is sealed with fluororubber double lips, fully adapting to the special environment of high humidity and high water mist in underground pump rooms.
Layout and Explosion proof Adaptation Optimization:
The diesel engine is horizontally arranged in the safe area of the pump room on the ground. After turning 90 degrees through the H-series right angle gearbox, it drives the vertical long axis fire pump vertically. The total axial height of the unit is reduced from 3.3m to 1.7m, completely solving the problem of insufficient lifting space in the underground pump room.
All electrical monitoring components of the supporting models in the chemical industrial park meet the Exd II CT4 explosion-proof level requirements, and all power components are located in the ground explosion-proof safety zone, completely avoiding the explosion risk of flammable and explosive media entering the electrical components, and fully complying with the fire and explosion prevention regulations of the petrochemical industry.
✅ Actual testing effect of project implementation
After the fire protection system was put into operation, it passed the annual acceptance of the fire department for 5 consecutive years, and its performance indicators far exceeded the national regulatory requirements
Emergency response speed meets the standard: the combination of diesel engine drive and H-series right angle gearbox, the pump set only takes 2.8 seconds from receiving the fire alarm signal to reaching the rated pressure, far below the 5-second upper limit required by GB6245 fire pump standard. It can still start 100% reliably in the event of complete power interruption, completely eliminating the risk of power failure in firefighting.
Significant improvement in reliability: The heavy-duty thrust bearing of the gearbox fully supports all axial loads of the pump, and the shaft vibration value remains stable below 2.5mm/s. The continuous fault free operation time of the equipment has been extended from 10 months to 60 months, and the backup reliability of the fire protection system has been improved to 99.99%. There have been no unplanned failures for 5 consecutive years.
The operation and maintenance efficiency has been greatly improved: after the total height of the unit has been significantly reduced, daily maintenance can be directly carried out using the conventional crane in the pump room for lifting. The dismantling and maintenance time of a single pump body has been reduced from 72 hours to 6 hours, and the downtime for maintenance of the fire protection system has been reduced by 90%, greatly reducing safety hazards during the fire window period.
Compliant operation in explosion-proof scenarios: The pump units in the explosion-proof area of the chemical park have been running continuously for 5 years without any electrical seal failure or medium leakage risks. They have successfully passed multiple explosion-proof safety inspections by the emergency management department and become a benchmark demonstration project for the local petrochemical industry's fire protection system.
📌 Summary of core project experience
When selecting the fire protection system, the maximum axial thrust of the pump must be taken as the core selection basis. It is prohibited to directly choose a regular right angle gearbox with the same power. Customized H-series models with upgraded high thrust bearing must be selected, with more than 30% axial thrust redundancy reserved to ensure the reliability of instant high torque starting of the fire pump.
In the scenario of diesel engine driven fire pumps, a mandatory fuel injection lubrication system must be installed, and the use of basic splash lubrication structures is prohibited to avoid early pitting and wear caused by insufficient lubrication of the tooth surface under instantaneous full load impact, resulting in transmission failure at critical moments of fire protection.
This solution can be directly replicated and promoted to special fire protection scenarios with limited space and extremely high safety requirements, such as underground fire pump rooms in super high-rise buildings, petrochemical and chemical explosion-proof parks, and large tunnel fire protection. It is currently the mainstream technical route for fire protection systems to meet high reliability emergency requirements.
Project Background:
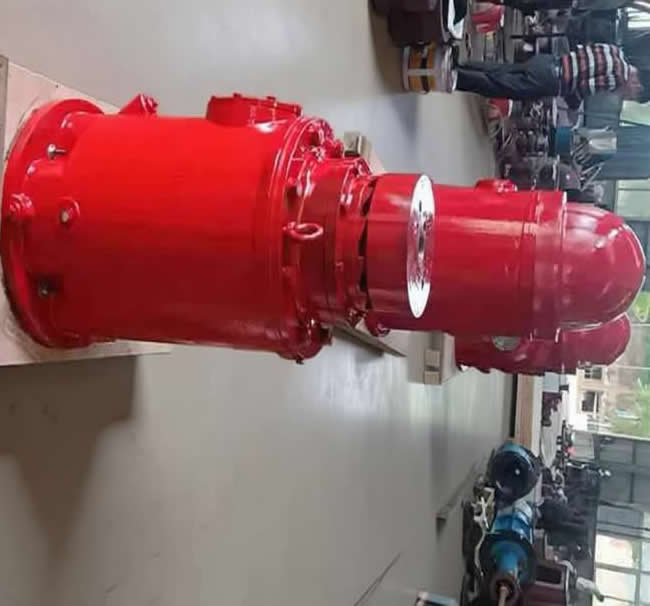
A certain enterprise undertakes the export of six vertical long shaft fire turbine pumps, matched with H-series right angle gearboxes, for large-scale fire protection systems.
Technical points:
·Pump type: Vertical long shaft fire turbine pump
·Supporting: H300 series right angle gearbox
·Application scenario: Large buildings/industrial fire protection
·Special requirements: The fire pump must meet NFPA standards, requiring instantaneous start-up and high reliability
Analysis:
Fire pumps have extremely high requirements for start-up response speed and reliability. Advantages of using a right angle gearbox solution:
1. Quick matching: A high-speed diesel engine can be selected as the prime mover, and the speed can be reduced to the required speed of the pump through the gearbox
2. Compact structure: saves installation space in the limited space of the fire pump room
3. Axial force treatment: The impeller of the long axis fire pump generates a huge axial thrust, which can be directly supported by the thrust bearing design of the H-series gearbox.
Previous:Structural characteristics of H-series right angle gearboxes
Next:Why choose the H series right angle gearboxes instead of direct drive for the pump?
Related Recommendations

Service hotline
screenshots ,WeChat Scan the Qr Code
WeChat:ljpump6666